In respect of importers of medical consumables, distributors of PPE (Personal Protective Equipment) and hospital supply chain procurement managers, packaging has become a critical element of international healthcare product sourcing. Once buyers acquire various disposable medical products from the same vendor, not only product quality or unit price becomes a factor. What else is important for them is the ability to use a reliable SKU management, storage, proper labeling, and market-ready appearance solution.
A professional OEM medical consumables packaging solution helps distributors organize different products under one purchasing program while maintaining product identification and shipment efficiency. This is especially important for companies serving healthcare markets in the United States, Germany, the United Kingdom, France, the Netherlands, UAE (Dubai), and Australia, where packaging requirements, labeling rules, and distribution models can vary significantly. Through customized private label PPE packaging, suppliers can also help distributors build their own healthcare brands with consistent product information, customized labels, and professional outer carton designs.
For many medical supplies distributor companies, a practical mixed SKU carton strategy can reduce inventory pressure, improve container utilization, and simplify regional distribution. Instead of receiving separate cartons for every product type, distributors can combine related medical consumables according to customer demand while maintaining clear traceability and packaging control.
Why OEM Medical Consumables Packaging Is Important for Medical Supplies Distributor Companies
The logistics for medical supplies require greater flexibility when compared to those of consumer goods. Medical establishments usually buy many different types of disposable products at once. Thus, it is important to design packaging that would meet these two criteria at once.
Supporting Multi-SKU Purchasing and Distribution
A typical distributor of medical products might be dealing with dozens or even hundreds of variations of goods like disposable masks, surgical gowns, isolation gowns, protective wear, caps, shoe covers, and other consumables in the healthcare industry. When all products are packed individually without taking into account the distribution considerations, logistics becomes more difficult.
The properly designed OEM medical consumables packaging strategy enables the supplier and distributor to make the optimal packing strategy according to the sales channel. For instance, the distributor who delivers goods to hospitals needs big boxes, but the channel selling through pharmacies or clinics requires small boxes.
Mixed SKU carton is not just about placing various products in one box. It is about the careful planning of the amount of product, available space in the carton, protection considerations, and identification strategies for various SKUs.
Improving Private Label PPE Packaging Programs
Private label PPE packaging is important for brand creation by corporations that are creating their own healthcare brands. Typically, private labeling will consist of product labeling, inner packaging, outer cartons, product manuals, and shipment labels rather than just the corporation logo.
If the intended target market is international, then the private label PPE packaging should suit the target market needs. In the case of a distributor selling PPE products in Germany and France, there will be a need for multi-language labeling. The US or Australian customers might be more interested in barcode systems and product information.
OEMs typically have experience in offering custom packaging design, artwork verification, labeling, and product documentation for new distributors.
Reducing Inventory and Warehouse Risks
Purchasing mixed products brings new difficulties into the process of inventory management. Inaccuracy in information about cartons, confusing SKU labels, or quantities will lead to extra expenses while receiving and fulfilling orders.
A good carton with mixed SKUs needs to include information about product categories, quantities, batches, and packaging format. This way, warehouse employees will be able to find products faster and avoid mistakes in order preparation.
For hospitals and healthcare systems, the information about packaging is equally important as there will be several departments that will receive these products.
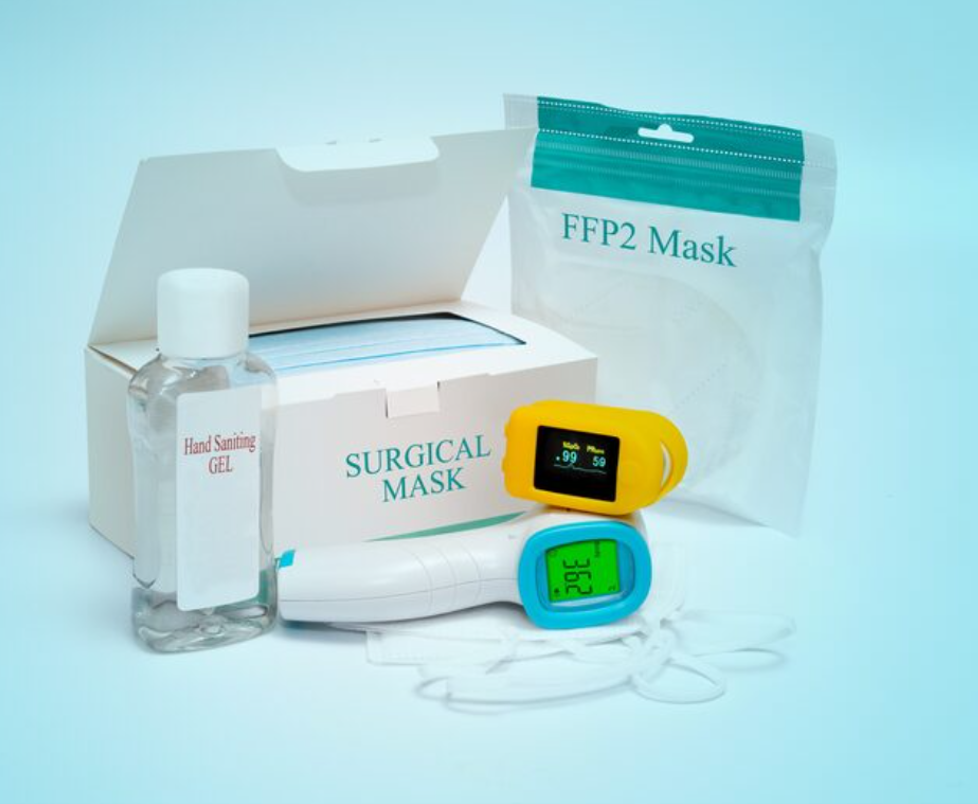
How to Design a Mixed SKU Carton for Medical Consumables
It will be necessary to have coordination between the buyer and supplier before large-scale manufacturing of such SKUs can be done. It is important that the medical importers should determine the packaging requirements at the product design phase.
Define SKU Combination and Carton Structure
Step one involves deciding on which products will go into a single carton. The buyer must provide a clear list of SKU, which should include product name, size, quantity, type of packaging, and the number of orders.
For instance, a PPE supplier can ship various sizes of disposable gowns and masks to meet regional requirements. It is important to ensure that the products can coexist in one carton without compromising their protection and identification.
When making quotations, buyers need to obtain all details of the carton packaging, including the number of boxes inside each master carton, carton sizes, and packing process.
Select Suitable Inner Packaging Formats
Medical consumable inner packing is the key to product protection, storage efficiency, and user convenience. The needs of packaging are different for various products based on the structure of materials and conditions of use.
In case of disposable PPE products, inner packing such as a bag, an inner box, or sealed packing increases hygiene standards and helps to distribute products easier. Small inner packing can be useful in hospitals for the control of consumption by departments.
For the assessment of OEM medical consumable packaging, it is necessary to verify the materials of inner packing, sealing, printing, and storage possibilities.
Optimize Outer Carton Marks and Shipping Labels
Outer cartons are the initial source of information for transport and warehouse receiving purposes. Outer carton marking provides assistance to logistics personnel in identifying the product and ensuring that the shipment documents coincide with the actual product.
Full carton marking includes product name, SKU, quantity, batch number, manufacturing data, destination information, and special handling requirements, if any.
In the case of international shipping, carton marking should conform to the purchase order, packing list, and other regulatory documents to prevent problems at customs clearance.
What Buyers Should Check During the 4. Quotation and Sampling Stage
This is the process where the medical importers can detect any possible danger prior to purchasing large quantities of the products. In place of considering only the aspect of price comparison, the importers need to consider specifications, packing capabilities, quality controls, and delivery reliability.
Confirm Product Specifications and Packaging Requirements
An ideal RFQ should contain product requirements. It is important to ensure that the product requirements as well as packaging requirements are confirmed at the same time for OEM medical consumable packaging since both affect cost and delivery.
The following details need to be confirmed in the specification sheet: material, size, weight, number of packaging per box, label design, carton design, and market requirements.
Evaluate Samples Beyond Product Appearance
The sample evaluation process needs to encompass the product as well as the packaging system. Consumers need to make sure that the sample is an accurate depiction of production capacity.
As far as private label PPE packaging goes, the sample review needs to take into account logo printing, label correctness, package strength, barcode readability, and presentation.
Consistency in packaging becomes an especially important factor for a medical supplies distributor.
Compare Supplier Quality Systems and Delivery Capability
Supplier comparisons need to encompass the manufacturing ability, documentation process, quality inspection processes, and stability of production.
ISO 13485 quality system, batch traceability processes, and export documentation capability can assist in decreasing the risks of procurement. Numerous OEM suppliers will be able to provide support for product customization, packaging, labeling, and other documents required in international markets.

Supplier Comparison for OEM Medical Consumables Packaging Projects
Choosing the correct supplier is one of the most important decisions for distributors building long-term healthcare supply programs.
Standard Supplier vs OEM Packaging Partner
The typical supplier may supply existing products that have limited packaging options. This solution may be appropriate in case of simple procurement needs, but it can be difficult for distributors trying to establish their own brand identity.
With an OEM packaging partner, you will be able to enjoy a broader spectrum of services, which include customizing your products, labeling your PPE packaging, mixing boxes, and adjusting packaging to the needs of a specific market.
For distributors operating in multiple countries, this flexibility can improve product competitiveness and simplify brand management.
Low Price Supplier vs Quality-Focused Manufacturer
Price matters, but healthcare procurement involves the evaluation of future costs. Errors in packaging, labeling and product specifications may lead to higher operational costs.
It is essential for a company to be able to provide information about manufacturing processes, testing and tracing, which will assist distributors in providing hospitals with their orders on time.
Short-Term Vendor vs Long-Term Supply Partner
A reliable OEM supplier should be able to cater to follow-up orders, new packaging needs, and potential product lines in the future. It is particularly crucial for distributors who are planning on creating their own healthcare brand names.
Working together long term enables suppliers to know more about the needs of their customers and ensure uniformity in products and packaging.
OEM Medical Consumables Packaging RFQ Checklist
Before sending an inquiry, medical buyers should prepare the following information:
- Product category and complete SKU list
- Product specifications and size requirements
- Target sales market
- Required certifications and documents
- Private label PPE packaging requirements
- Logo, artwork, and label specifications
- Inner packaging format
- Mixed SKU carton combination plan
- Carton dimensions and shipping requirements
- Barcode and carton mark requirements
- Sample approval process
- Production lead time and delivery schedule
- Expected repeat order volume
A detailed RFQ allows suppliers to provide more accurate quotations and helps buyers compare different manufacturers more effectively.
Conclusion
For global suppliers of medical consumables, PPE, and hospital procurement managers, packaging is an important factor affecting their supply chain. With a good OEM medical consumables packaging service, you will be able to achieve better inventory management, use your own brand name for packaging of PPE, and have an option of using mixed SKU carton solution for international shipping.
Through the analysis of specifications, samples, carton designs, and capabilities of potential vendors at the quotation stage, you will be able to minimize your purchasing risks and create a stable healthcare supply chain. To explore more OEM medical consumables packaging solutions, private label PPE packaging options, and customized medical supply manufacturing services, visit Medical,pet,hotel,beauty non-woven supplies & scrub suits – GUANG ZHOU SHIJINGCHENG NON-WOVEN PRODUCTS CO.,LTD.